Choosing Stainless Steel Castings in 2026 takes more than comparing prices or selecting the grade with the highest chromium content. The right choice depends on where the part will work, how it will be made, and what failure would cost. A pump housing exposed to salty water has different needs from a food-processing valve washed daily with cleaning chemicals. Small details matter: wall thickness, machining allowance, surface finish, and the shape of internal passages.
Casting expert John Campbell’s published work emphasizes controlling metal filling and solidification to improve casting quality. Put simply, sound parts start inside the mold. That principle makes supplier questions important: Which grade and casting process suit the design? How are shrinkage, porosity, and dimensional variation checked? Can the foundry provide material test reports and inspection records? Ask for evidence, not just assurances. A polished sample is useful, but it cannot prove consistent production.
This guide will help buyers compare stainless grades, casting methods, quality controls, and supplier capabilities. It will also consider cost across the part’s service life, not just the initial quotation. No checklist removes every trade-off. A specification can be too demanding, too vague, or simply copied from an older project. Review the actual operating conditions, then confirm critical requirements with the foundry and a qualified materials engineer. Good decisions are specific. Sometimes, the uncomfortable answer is that more testing is needed before ordering.
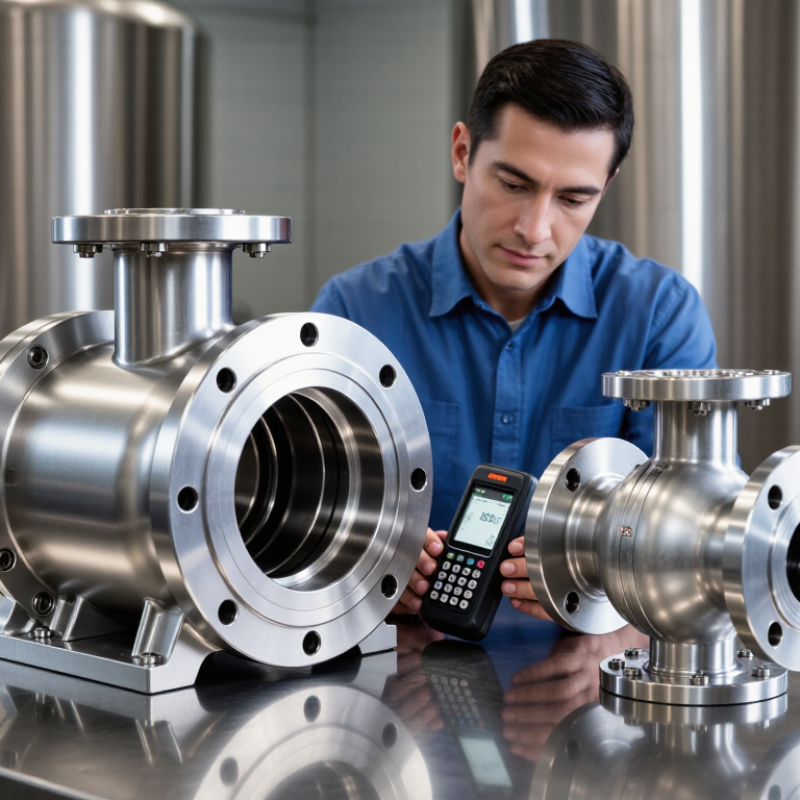
Before selecting a stainless steel casting, define what the component must withstand. Record the working temperature, pressure, fluid chemistry, chloride exposure, cleaning method, and expected service life. A valve body handling warm saline water faces different risks from a pump casing in a dry plant. Small details matter. Note peak conditions, not only normal operation; short temperature spikes can change material and inspection requirements.
The NACE IMPACT study estimated corrosion costs at US$2.5 trillion worldwide, or 3.4% of global GDP, underscoring the value of matching material to environment. For castings, compare candidate grades against the actual corrosion, strength, and temperature requirements, then confirm applicable specifications, such as ASTM A351 for pressure-containing stainless steel castings. Also define loads, wall thickness, machining allowance, surface finish, and inspection needs. These affect both casting design and acceptance. A smooth surface may be essential in a washdown line, while a rougher finish may suit a hidden support. It is easy to overlook start-up and shutdown conditions. The first requirement list may still miss them, so review it with the casting engineer before requesting quotations.
How to Choose Stainless Steel Castings in 2026?
Compare Stainless Steel Grades and Their Properties
Choosing a casting grade starts with its working environment, not its label. Grade 304 offers useful corrosion resistance for indoor equipment, food-handling components, and general-purpose parts. It is widely used, but chlorides can cause pitting, especially in warm, salty conditions. Grade 316 adds molybdenum, which improves resistance to chloride attack. That can matter for coastal fittings or washdown equipment. It does not make the casting immune to corrosion. Not quite.
For higher strength and wear resistance, a duplex grade such as 2205 may suit pressure-containing parts or demanding process equipment. Its mixed austenitic-ferritic structure can provide greater strength than common 300-series grades, but casting quality and heat treatment need close control. For hot service, compare grades by their strength at operating temperature, not just room-temperature data. Ask for test results relevant to the part, including chemistry, tensile properties, and inspection records. A polished sample can look reassuring while hiding shrinkage or inclusions inside. I have seen this comparison become less tidy once wall thickness, machining, and service conditions enter the discussion. Specify those details before approving a grade.
| Cast Grade | Common Wrought Equivalent | Typical Composition Characteristics | Typical Minimum Tensile Strength | Typical Minimum Yield Strength | Corrosion Resistance | Weldability and Fabrication | Common Uses | Selection Considerations |
|---|---|---|---|---|---|---|---|---|
| CF8 | Type 304 | Approx. 18% chromium and 8% nickel; a general-purpose austenitic stainless casting grade. | 485 MPa (70 ksi) | 205 MPa (30 ksi) | Good resistance in many atmospheric, food-processing, and mildly corrosive environments. Not ideal for sustained exposure to warm chloride solutions. | Generally good. Use suitable filler and procedures; control heat input and assess sensitization risks for the service conditions. | Pumps, valves, housings, food-processing equipment, and general-purpose fluid-handling components. | A practical starting point for general corrosion resistance when strong chloride resistance is not required. |
| CF8M | Type 316 | Approx. 16–18% chromium, 10–14% nickel, and 2–3% molybdenum. | 485 MPa (70 ksi) | 205 MPa (30 ksi) | Usually better than CF8 in chloride-containing and many mildly acidic environments because of its molybdenum content. It is not immune to pitting or crevice corrosion. | Generally good, although molybdenum-bearing filler and appropriate welding procedures may be needed for welded repairs or assemblies. | Marine and chemical-process pumps, valve bodies, fittings, and equipment exposed to more aggressive fluids. | Consider when the service fluid is more corrosive than CF8 can reliably handle; verify chloride concentration, temperature, and crevice conditions. |
| CF3M | Low-carbon Type 316 (316L) | Low-carbon molybdenum-bearing austenitic casting grade; carbon is limited to help reduce weld-related sensitization. | 485 MPa (70 ksi) | 205 MPa (30 ksi) | Similar general corrosion resistance to CF8M, with improved resistance to intergranular corrosion after welding when used and processed appropriately. | Good for welded construction and repair. Welding procedure qualification is still important, especially for thick sections and corrosive service. | Welded pump and valve components, chemical equipment, and cast parts requiring post-cast welding. | Choose over CF8M when welding or intergranular corrosion after welding is a key concern; it does not eliminate chloride pitting risk. |
| CA6NM | Modified 13% chromium martensitic stainless steel; no direct one-to-one equivalent | Typically about 11.5–14% chromium, with nickel and a controlled carbon content; supplied in a heat-treated condition. | 760 MPa (110 ksi), typical specified minimum for common heat-treated condition | 550 MPa (80 ksi), typical specified minimum for common heat-treated condition | Moderate resistance in suitable water and mildly corrosive environments. Generally less resistant to many corrosive media than CF8M. | Weldable with careful procedure control and appropriate preheat, filler, and post-weld heat treatment as required by the specification and application. | Hydraulic turbine components, pump parts, high-strength water-service components, and pressure-containing parts. | Useful when strength, toughness, and erosion resistance are priorities; confirm heat treatment, impact requirements, and actual water chemistry. |
| CB7Cu-1 | 17-4 PH family; cast precipitation-hardening stainless steel | Chromium-nickel-copper precipitation-hardening alloy; final properties depend strongly on solution treatment and aging condition. | Varies by heat treatment and applicable specification | Varies by heat treatment and applicable specification | Good resistance in many atmospheric and mildly corrosive environments, but generally not a substitute for CF8M in severe chloride service. | Machining and welding considerations depend on the condition and procedure. Heat treatment after fabrication may be necessary to achieve target properties. | High-strength pump, valve, and mechanical components requiring a combination of strength and corrosion resistance. | Specify the required heat-treatment condition and mechanical properties on the purchase documents; compare corrosion conditions before selecting. |
Note: Mechanical-property figures are representative specification minimums for common casting grades and conditions, not guaranteed values for every casting. Actual requirements depend on the governing ASTM or equivalent specification, product form, section thickness, heat treatment, testing, and purchase order. Confirm the exact grade, material certificate, and service conditions with the casting supplier and design engineer.
How to Choose Stainless Steel Castings in 2026?
Selecting the right casting process starts with the component’s shape, service conditions, and production volume. Investment casting suits thin walls, complex passages, and tight dimensional requirements. It can reproduce a small impeller with curved blades more accurately than ordinary sand casting. Sand casting remains practical for larger housings, simpler geometry, and lower annual quantities. The surface may be rougher, but machining can correct critical faces.
Design decisions often determine quality before melting begins. Keep wall thickness as even as possible to reduce shrinkage and distortion. Add generous fillets around corners. Avoid deep, narrow pockets that trap sand or complicate pattern removal. A casting engineer should review draft angles, gate locations, risers, and machining allowances together. A 2 mm allowance may be excessive for one feature and insufficient for another.
Small details matter.
Stainless steel grades also influence process selection. High-alloy materials may require controlled melting, clean molds, and careful heat treatment. Ask the foundry to verify chemical composition through material testing. Dimensional inspection, visual checks, and suitable non-destructive testing can reveal cracks or internal defects. In production reviews, I have seen attractive prototypes fail because the drawing ignored tool access. That mistake is avoidable, though design teams sometimes prioritize appearance too early. Request trial castings before approving full production. Measure distortion after heat treatment, not only before it. Real parts often disagree with elegant computer models.
Select the casting process according to the required wall thickness, dimensional complexity, surface finish, and production volume.
The chart shows typical minimum wall-thickness ranges used for stainless steel castings. Investment casting is generally preferred for thin, detailed components; sand casting suits larger and less intricate designs; centrifugal casting is commonly selected for rotational parts such as rings, sleeves, and tubes. Actual limits depend on alloy grade, geometry, tooling, and foundry capability.
Choosing stainless steel castings requires more than comparing prices. Begin with the casting’s service conditions, including temperature, pressure, corrosion exposure, and loading cycles. Ask for chemical composition reports from each heat. Verify carbon, chromium, nickel, and molybdenum levels against the specified grade. Small chemistry changes can affect weldability and corrosion resistance.
Quality evidence should include tensile results, hardness readings, dimensional reports, and agreed non-destructive testing. Radiography can reveal shrinkage, while dye penetrant testing can expose surface cracks. Check whether reports identify the heat number and inspection date. A certificate without traceability is weak evidence. Standards such as ASTM, EN, or ISO may guide acceptance, but the purchase specification must define the actual requirements.
Supplier capability deserves equal attention. Review furnace capacity, pattern control, heat treatment records, machining equipment, and corrective-action procedures. Ask to see sample inspection plans. A capable supplier can explain what happens after a failed test, not merely promise perfection. Visit the production area when possible. Look for clean identification tags, protected castings, and records that match the physical parts. No supplier gets every detail right. I would question any factory showing flawless paperwork but no documented nonconformities. A realistic supplier admits limits, tracks recurring defects, and improves the process before shipment.
Balance Total Cost, Lead Time, and Long-Term Performance
A low quotation can hide costs in machining, inspection, and replacement. Compare the delivered casting, not just its price per kilogram. Ask suppliers to quote the same alloy, tolerance, surface condition, and test plan. Then check whether their lead-time estimate includes tooling, sample approval, and production inspection. Small details matter. A delayed pump housing can cost more than a modest price difference if it stops a production line.
Long-term performance depends on the service environment. Chlorides, temperature swings, and repeated loading can change which stainless grade is suitable. Review corrosion test results and traceability records, and ask how defects are handled. The World Steel Association reported global crude steel production of 1,882.6 million tonnes in 2024, illustrating the scale of steel supply—but not guaranteeing availability of a particular casting grade or shape. Verify capacity directly. For environmental context, the International Energy Agency estimates iron and steel production accounts for around 7% of global energy-related CO₂ emissions. That figure covers the broader sector, not a specific casting; still, scrap use, yield, and rework are worth discussing. I would not assume the lowest-carbon option is automatically the best value. Compare documented performance with realistic maintenance and replacement needs.